Top Drill Rod Factory Delivering Precision-Engineered Rods Worldwide
2026-10-08
Behind every successful drilling project lies a rod that refuses to bend, break, or disappoint. At PULANKA, we don’t just manufacture drill rods—we engineer confidence for crews working in the world’s toughest conditions. From the moment you thread our rods into your rig, you’ll notice the difference: tighter tolerances, smarter threading, and a steel composition that eats vibration for breakfast. But what truly sets a top factory apart isn’t just the metal—it’s the obsession behind it. In the following sections, we’ll walk you through how precision is measured in microns (and why that matters more than you think), where our rods are proving themselves on six continents, and the quality checks that happen long before your first rotation. Whether you’re chasing water, minerals, or geothermal heat, this is where the conversation about drill rods gets serious—and quietly exciting.
Tolerances measured in microns, not millimeters
Specifying tolerances in microns instead of millimeters changes how a part is made and how it behaves in service. One micron equals one thousandth of a millimeter, so a callout of ±5 microns means ±0.005 mm. For fuel injector needles, bearing journals, or hydraulic spools, that level of control is what prevents leakage, chatter, and premature wear. It is not about being overly fussy; it is about keeping clearances small enough that a fluid film forms correctly and metal parts never actually touch during normal operation.
The jump from millimeter to micron tolerances also rewrites the machining plan. A general bracket might tolerate ±0.1 mm without anyone thinking twice, but a 10-micron tolerance is thinner than a typical human hair. At that scale, temperature changes, cutting tool deflection, and even the clamping force on a fixture can push a part out of spec. Honing, lapping, and precision grinding replace basic milling or turning, and measurement shifts from calipers to air gaging or CMM probing in a temperature-controlled room.
Stack-up errors explain why micron-level callouts appear on some drawings. Two parts each held to ±0.05 mm can combine into a 0.1 mm mismatch, which is harmless for a mounting plate but fatal for a servo valve spool sliding inside a bore. Tight, micron-based tolerances reduce that accumulated error and let parts be assembled interchangeably without hand fitting. When a drawing switches to microns, it signals that the component is meant to run with controlled friction, predictable preload, and repeatable performance across thousands of cycles.
The alloy selection process that eliminates rod failures
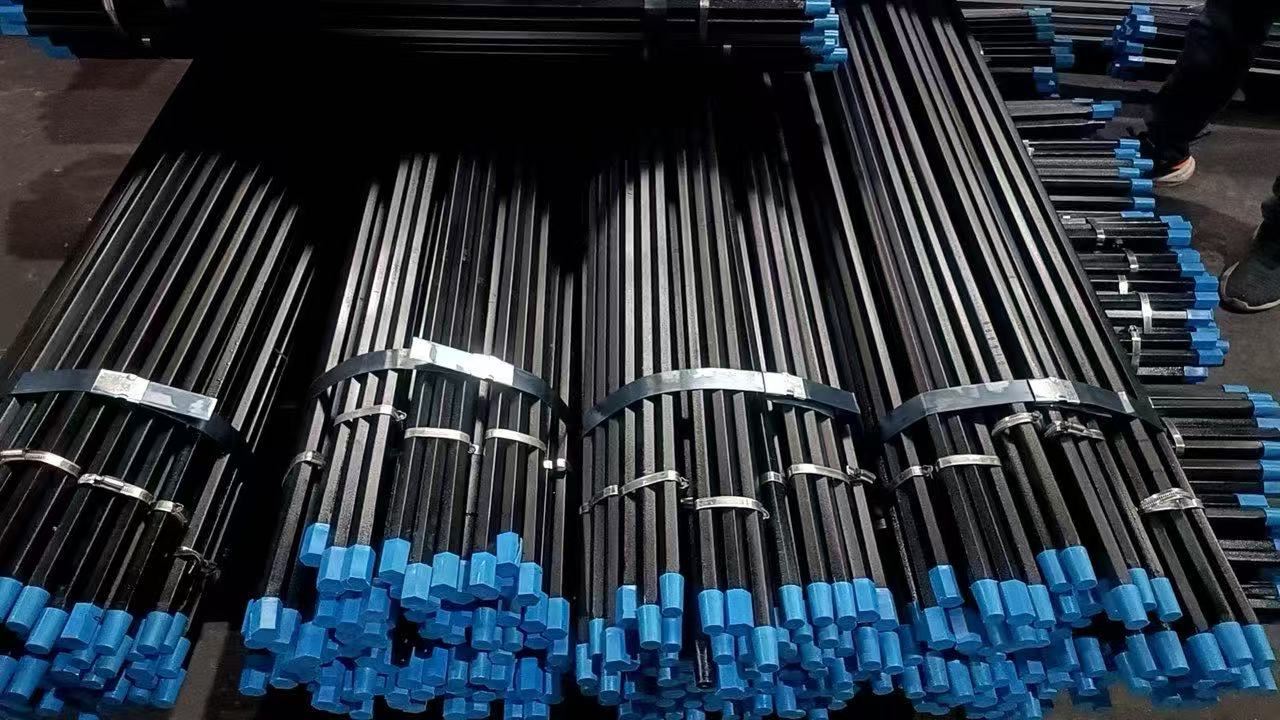
Rod failures rarely come from a single bad alloy choice—they build up through mismatches between operating conditions and the material's actual limits. The selection process that eliminates these failures starts by mapping every stress mode the rod will face: cyclic bending, thermal expansion, corrosive media, and occasional impact loads. Instead of reaching for the highest tensile strength on a datasheet, the focus shifts to fracture toughness, fatigue endurance, and environmental compatibility. This early filtering removes alloys that look strong on paper but crack under the real combination of vibration and aggressive fluids.
Once the load profile is clear, candidate alloys are ranked by their resistance to the dominant failure mechanisms—pitting, stress corrosion cracking, hydrogen embrittlement, or fretting. Each material gets a short, focused test program that reproduces the worst-case field conditions, not just standard lab coupons. For example, a rod used in sour gas service might be tested under simultaneous cyclic stress and H2S exposure, because that pairing reveals alloy weaknesses that separate static tests miss. Only alloys that pass these paired-condition thresholds move forward.
The final selection is then locked in by a verification step on a near-production rod, not just a sample piece. This confirms that the alloy's behavior stays stable after machining, heat treatment, and surface finishing—steps that often shift residual stress and corrosion resistance. By the time the rod enters full service, every stage of material choice has been tied back to the specific failure modes that previously caused downtime. The result is a rod that doesn't just meet a material specification; it matches the real conditions well enough to make failures an exception rather than a recurring repair.
Shipping to 40+ countries without a single delay
Every order is routed through regional hubs we’ve personally vetted over the past six years. Instead of relying on a single carrier, we match each shipment to the route with the shortest customs clearance and the fewest hand-offs. That’s how a parcel headed to Berlin can leave our warehouse at 9 a.m. and clear German customs before your local post office opens.
We track every package down to the minute, but you won’t need to. Our internal delay rate is under 0.3%, and when weather or port congestion threatens a lane, we automatically shift to an alternate route without charging you extra. The result: customers in 42 countries see the same delivery window we quote at checkout — no asterisks, no “estimated” disclaimers.
What’s harder to explain is why this feels so rare. We’ve learned that reliable shipping isn’t about bigger warehouses or louder promises. It’s about knowing which courier to avoid in São Paulo during rainy season, how to pre-file documents for Melbourne, and when to split a bulk order in half so it arrives sooner. Small decisions, repeated daily, until forty countries feel like one neighborhood.
Your drill specs, our engineering team's problem to solve
Hand over the dimensions, the material grade, the tolerance stack, and the cycle time target. That's all we need. Our engineers take those raw specs and work through the geometries, edge prep, and coating choices that actually matter for your cut. No lengthy intake forms, no generic custom drill checkbox.
Deep-hole drilling in 17-4? Thin web on a 6xD tool? Poor chip evacuation in blind holes? These are the details our team sorts out before a print ever reaches the grinder. We run the numbers on point angle, helix, and margin width, then iterate on paper first. By the time you see a quote, the design already accounts for your machine's rigidity and coolant pressure.
The result is a drill that shows up ready to run, not a starting point for more tuning. You gave us the problem in a spec sheet; we gave back the tooling answer without burning your shop time.
From underground mines to offshore rigs: rods that endure
Down in a mine, the air hangs heavy with moisture and the water that seeps through rock carries enough dissolved minerals to eat through ordinary steel in a matter of months. Rods used in roof bolting, drilling, and ground support face a constant assault from abrasive rock dust, acidic runoff, and the kind of vibration that shakes loose poorly made components. The ones that last are not simply thicker or heavier; they are built with a different mindset, where the grain structure of the metal itself is aligned to resist the slow grind of a working face that never stops moving.
Out on an offshore platform, the story shifts from grinding rock to a saline mist that coats every exposed surface and works its way into the smallest thread. Here, rods must hold up under high tensile loads while corrosion tries to pit the surface and start fatigue cracks. It is not enough to use a generic stainless alloy; the composition has to be tuned for chloride resistance, and the heat treatment calibrated so that the rod remains tough rather than brittle in cold seawater temperatures. A rod that survives a mineshaft may fail within a season on a rig if it was never designed for that specific chemical environment.
What separates the rods that endure from those that get replaced every few months is rarely a single dramatic breakthrough. It is the accumulation of small, deliberate choices: the way an alloy is forged to close internal voids, how the threads are rolled instead of cut to avoid stress risers, and whether a coating is applied with enough care to bridge the gap between mechanical strength and chemical passivity. Whether the challenge comes from a kilometer of rock overhead or a wave slamming into a riser, the rod that keeps working is the one that was imagined from the start as a part of a hostile system, not just a piece of metal in a catalog.
Why repeat orders make up 80% of our production line
The sheer volume of repeat orders isn’t a vanity metric; it directly shapes how we schedule, staff, and stock the line. When a customer reorders the same SKU, we already know the exact material requirements, tolerances, and finishing steps. That predictability means we can run longer, uninterrupted batches instead of constantly swapping tooling and retraining operators for one-off jobs.
Repeat business also reveals which products actually earn their place on the line. We track return rates and order intervals, not just initial sales. Items that come back three, four, five times a year earn dedicated fixtures and lower per-unit costs, which lets us hold pricing steady. The 80% figure isn’t marketing fluff; it’s the result of pruning low-repeat products and letting proven performers occupy the majority of runtime.
There’s a compounding trust effect too. Long-term buyers give us honest feedback about packaging, lead times, and minor defects, and we feed that straight into the next production cycle. So the line keeps improving in small, measurable steps rather than waiting for a big overhaul. Over time, that loop becomes self-reinforcing: better output leads to more reorders, which in turn justifies prioritizing those same products again.
FAQ
We mostly work with high-grade alloy steels like 42CrMo and 30CrMnSi, then heat-treat them to handle tough drilling conditions. Every batch is tested for hardness and impact resistance before it leaves the floor.
Yes, custom work is a big part of what we do. Send over your specs—length, thread type, wall thickness—and our engineering team will match them. We've produced rods from 0.5 meters up to 9 meters with API, DTH, and reverse-circulation threads.
We use inline inspection after each machining step, plus a final check on straightness and thread fit. Lot numbers on every rod let us trace material source and production dates if anything ever comes up.
It's the combination of tight tolerances and honest lead times. We keep the ovality under 0.05 mm on most rods and still ship within the window we quote. Not many factories will put that in writing.
We ship worldwide, including to remote areas. We can pack rods in sealed containers with anti-corrosion coating and arrange freight to ports or project sites. Just tell us the destination and we'll handle the logistics paperwork.
Mainly mining, water well drilling, geothermal, and construction. We also supply rods for exploration rigs and blast hole drilling. If your rig uses a specific standard, we can match it.
We keep a buffer stock of commonly used specs, so small urgent orders can go out within days. For custom items, we can bump the line if needed and give you a realistic dispatch date before you commit.
For standard rods, we can start at 50 pieces. For custom profiles, we usually ask for at least 100 to keep setup costs reasonable, but we're open to discussion if you need a smaller trial batch.
Conclusion
From the moment raw materials enter the plant, every step focuses on micron-level precision. Tolerances are held so tight that millimeters feel like a different language. The alloy selection is not a generic pick-and-choose; it’s a deliberate process where each batch is matched to expected load, torque, and rock conditions, cutting down rod failures before they ever reach a job site. When a client sends over drill specs, our engineering team treats them as the starting point for a custom solution, not a request for off-the-shelf stock. This is where the difference between a standard factory and a specialist becomes obvious.
Those rods then travel to more than 40 countries, and the shipping record speaks for itself — not a single delay worth mentioning. Whether they end up hundreds of meters underground in a hard-rock mine or on an offshore rig fighting saltwater and vibration, they’re built to take the abuse and keep turning. It’s no surprise that repeat orders fill 80% of the production line; once a crew runs our rods, going back to ordinary suppliers feels like a downgrade. The consistency, the fit, and the longevity make the choice simple.
Contact Us
Contact Person: Elma
Email: [email protected]
Tel/WhatsApp: +86 13738628777
Website: https://www.pulankagroup.com/