Pharmaceutical Air Compressor for 24/7 Continuous Operation Buying Guide
2026-08-21
In pharmaceutical manufacturing, every second of downtime can compromise product integrity and regulatory compliance. Choosing the right air compressor for 24/7 continuous operation isn't just about performance—it's about safeguarding your entire production line. This buying guide cuts through the noise, focusing on the critical factors that keep your cleanroom and processes running without interruption. Whether you're upgrading existing equipment or specifying a new system, Seize Air offers insights that help you avoid costly mistakes and ensure reliability where it matters most.
Why 24/7 Duty Ratings Fall Short
A generator stamped with a 24/7 duty rating suggests it can run around the clock without pause, but real-world conditions rarely mirror the controlled tests behind that label. Heat, altitude, dust, and fluctuating loads all chip away at the engine's true endurance. The rating often assumes a light, steady draw—not the sudden surges or prolonged heavy pulls that happen on a job site or during an outage. So while the badge sounds reassuring, it's more of a starting point than a guarantee.
Maintenance demands also get lost in the 24/7 promise. Oil changes, filter swaps, and cool-down periods are unavoidable, yet the rating rarely accounts for these interruptions. Push a unit past its practical limits week after week, and you'll see dropped efficiency, shorter service life, and even sudden failure. The label doesn't lie—it just leaves out the fine print about how often you'll need to stop and tend to the machine.
Fuel supply adds another wrinkle. Depending on tank size and load, a generator might drain itself in eight or ten hours, not twenty-four. Refueling means downtime, and no rating can conjure fuel from thin air. Smart buyers look beyond the badge and ask about duty cycle under real loads, cooling margins, and service intervals. That's where the actual story of reliability gets told.
Oil-Free Air Still Isn't Particle-Free
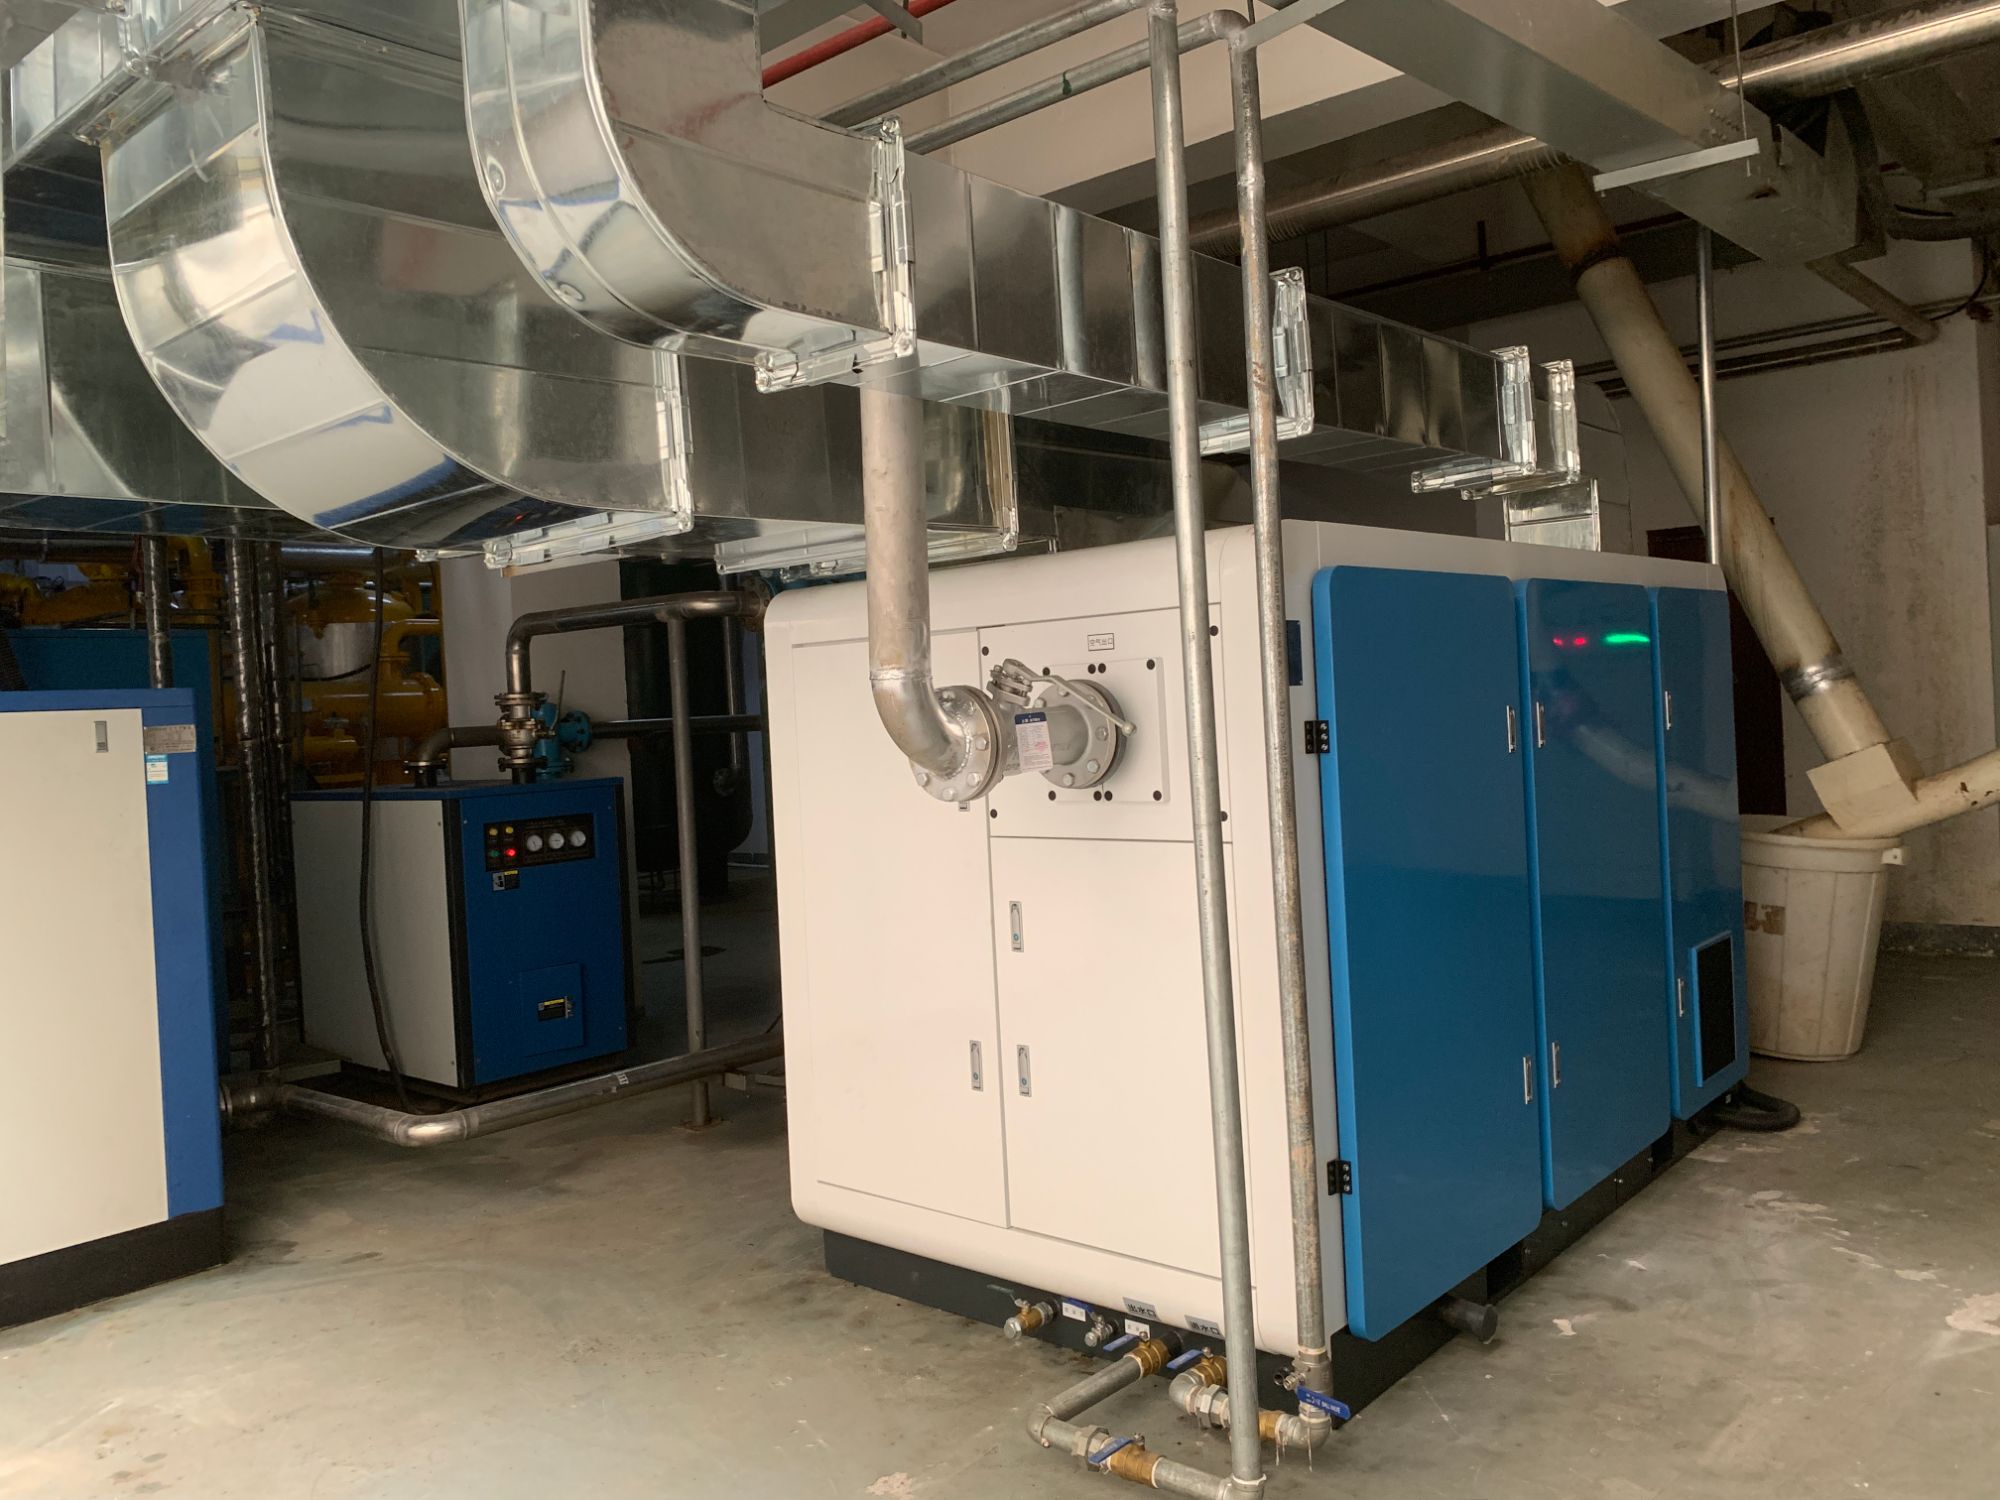
A compressor labeled oil-free only means the pump itself doesn't use oil in the compression chamber. That says nothing about what's floating in the surrounding air. Dust, metal shavings, moisture droplets, and even microscopic fibers from packaging or clothing all get pulled into the intake and pushed downstream. In many workshops, the air is far dirtier than the compressor's internal lubrication ever was.
Particles that bypass filtration don't just disappear. They lodge in pneumatic valves, erode seals, and contaminate sensitive end products. A single pinch of fine silica can ruin a spray finish or shorten the life of an air tool by months. The problem isn't theoretical, it's measurable with a basic particle counter on the discharge line.
Treat oil-free as one checkbox, not a complete answer. Upstream intake filters, downstream coalescing filters, and proper point-of-use drying matter just as much as the pump design. Without them, you're simply trading one contaminant for a cocktail of airborne debris.
Sizing for Load Spikes You Can Set Your Watch By
Predictable load spikes are less about guessing and more about reading a calendar. Payroll runs hit at 5 p.m. on the last weekday of the month. Open enrollment starts at midnight. A sports ticketing site sees traffic double the moment a playoff berth is clinched. Instead of treating these as surprises, map them against business events and historical request logs. If you can name the trigger, you can name the required headroom.
Once the pattern is pinned down, sizing gets simpler. Build for the spike, not for idle Tuesday mornings. That means pre-warming caches before a known rush, scaling read replicas in advance, and leaving enough write capacity for the rush itself. A good rule of thumb is to add twenty to thirty percent buffer on top of the highest observed peak from the last three cycles, then adjust after each run. You will still hit occasional anomalies, but the baseline stops being a gamble.
Redundancy Without Doubling the Utility Room
Achieving redundancy in a home utility setup often implies building a second dedicated room, but that approach eats up square footage and budget. A smarter strategy is to design the existing utility space with overlapping functions. For example, a fold-down ironing board, a wall-mounted drying rack, and a deep sink with a cutting board cover can turn the laundry corner into a temporary prep kitchen or pet washing station. When one task is blocked or the primary area is in use, the room simply shifts roles without requiring a duplicate footprint.
Another way to create functional backup is through movable storage and modular partitions. Instead of fixed cabinetry, use lockable rolling carts, stackable bins on tracks, and a retractable table that slides into a wall cavity. These elements let you quickly reconfigure the room for different loads—say, sorting bulky winter gear one day and staging a home repair project the next. The key is that every major utility function has a secondary, space-saving execution: a hanging garment rod above the washer doubles as a drying line, and a countertop extension over the appliances serves as both folding surface and gift-wrapping station.
This layered approach delivers the resilience of a second utility room without the construction cost or wasted hallway space. It also makes daily chores less frustrating because you are never locked into one rigid layout. By investing in multi-purpose fixtures and clever vertical storage, you create a room that adapts to unexpected demands—a burst pipe in the kitchen, a sudden need for a quarantine cleaning zone, or a weekend DIY project—while keeping the original footprint exactly the same.
Dew Point Stability Across Shift Boundaries
Operators often notice subtle shifts in dew point readings when moving from one production shift to the next, even if the same equipment and settings remain untouched. These variations rarely point to sensor drift alone. Instead, they usually trace back to how each crew handles purging cycles, door openings, or the timing of regeneration. Without a clear handoff log that captures these routine actions, the next shift inherits a mystery rather than a measurement.
A more useful approach is to treat dew point stability as a shared behavioral metric, not just a machine output. When outgoing and incoming operators review the trend line together for five minutes, they can spot patterns that single-shift reports miss—such as a slow climb after lunch breaks or brief dips tied to filter changes. Writing down the context behind the numbers makes the boundary less of a cliff and more of a bridge.
Some plants find that the most reliable fix isn't a new instrument, but a simple overlap in responsibility. If each shift records its last hour of data alongside the first hour of the next, anomalies become easier to attribute to a specific action or delay. That shared ownership keeps dew point curves from wandering every eight hours, and it turns handoff time into a chance to protect product quality instead of just signing a clipboard.
Maintenance Plans That Match Production Reality
Many facilities operate with maintenance schedules that look perfect on paper but collapse under real production pressures. The gap between planned downtime and actual line availability often comes down to one factor: whether the maintenance plan was built around a theoretical ideal or around the daily rhythm of the floor. An effective plan considers shift patterns, peak order periods, tooling changeovers, and the true condition of aging equipment—not just manufacturer-recommended intervals. By mapping maintenance tasks to the moments when machines are already idle or running below capacity, teams avoid unnecessary stoppages and keep throughput stable without sacrificing reliability.
Matching maintenance to production reality also means accepting that not every asset deserves the same level of attention. A high-volume packaging line may need weekly vibration checks and monthly gearbox inspections, while a backup conveyor used only during overflow can safely run on a condition-based schedule. The key is to categorize equipment by its actual role in current production flow, then align preventive and predictive tasks with that ranking. This approach reduces wasted labor on low-impact assets and directs skilled technicians toward the failures that would truly disrupt output.
Finally, a realistic plan stays flexible when production priorities shift. Instead of rigid calendar-based work orders, it uses triggers like runtime hours, output counts, or quality drift to determine the right moment for intervention. Morning meetings between maintenance and production leads become quick alignment sessions rather than conflict resolution. When the plan reflects how the plant actually operates—peak seasons, operator skill levels, and material variations included—compliance rises naturally, unplanned downtime drops, and the maintenance team spends less time defending the schedule and more time improving it.
FAQ
Look beyond the marketing label. The motor and airend should have a true 100% duty cycle rating at your maximum working pressure, not just intermittent bursts. Built-in aftercooling, oversized cooling fans, and thermal protection that actually derates output before failure are all signs it can hold up when run around the clock.
Not every zone demands it, but if the air contacts product, packaging, or critical instruments, oil-free Class 0 is the safest bet. Even with high-efficiency filtration, oil carryover can become a contamination risk over time, and that's a compliance headache you do not want during an audit.
A receiver should cover short peak demands without forcing the compressor to start and stop constantly. Size the dryer at least 10 to 15 percent above the compressor's maximum output, and account for the hottest expected inlet air temperature, not the ideal lab conditions.
Blocked intake filters, ignored condensate drains, and dirty coolers are the quiet killers. Another common issue is never checking the dewpoint trend. When moisture levels creep up in compressed air logs, it often means the dryer is overloaded or the compressor is running hotter than designed.
If your process cannot tolerate unplanned air loss, yes. A single compressor, no matter how well built, will eventually need service or trip on a fault. An N+1 setup with automatic switchover prevents batch loss. Even a smaller backup unit or a tie-in point for a rental compressor reduces the risk dramatically.
ISO 8573-1 is the practical baseline for setting limits on particles, water, and oil. For sterile or injectable areas, you will also need to map those classes to your own GMP risk assessment. Ask the supplier to match the dryer and filtration package to the specific class, not just the compressor alone.
Request specific power data in kW per 100 cfm at full load, 50 percent load, and no load. Compare those numbers across brands at the same discharge pressure. Also check if the unit offers heat recovery or a variable speed drive that actually reduces energy when demand drops, because a fixed-speed machine running unloaded still burns power.
Frequent high-temperature alarms, very short unloading cycles, fluctuating outlet pressure or dewpoint, and increased vibration or noise over time are all red flags. If the electrical current curve shows sharp spikes beyond normal motor draw, the compressor is likely working beyond its realistic thermal margin.
Conclusion
Most pharmaceutical plants discover too late that a compressor stamped '24/7 duty' is not the same as one engineered for continuous, unrelenting operation. Thermal stress builds up during long runs, and units rated for intermittent service will trip or wear out just when batch production cannot pause. True continuous-duty machines use oversized coolers, reinforced valves, and conservative motor sizing to handle the full load without cycling. At the same time, oil-free compression only solves part of the contamination puzzle: it removes lubricant from the air stream but does nothing for particles shed by piping, desiccant dust, or moisture carryover. Final filtration and drying must still be matched to ISO 8573-1 limits specific to your cleanroom class. Sizing also deserves more than a glance at average flow. Pharmaceutical processes often spike at predictable moments—CIP cycles, fluid bed drying, pneumatic conveying—so the compressor package should be built around the highest realistic simultaneous demand, not the mean. Redundancy can be achieved without doubling floor space by using duplex or variable-speed units that share a common control system; one machine can handle the baseline while the second picks up peaks or serves as a hot standby.
Dew point stability across shift boundaries is another overlooked failure point. When lines idle between shifts, cool surfaces collect condensation, and the first blast of morning air can carry liquid water into sterile areas. Drying systems need either thermal mass or fast-acting dew point control to hold a steady outlet condition during load swings. Maintenance planning has to respect that a 24/7 line rarely offers long shutdown windows. Look for condition-based monitoring, tool-free access to filters and valves, and remote diagnostics that flag wear before it becomes a production stop. The right buying decision weighs all of these factors together rather than treating the compressor as a standalone box. It is an integrated supply of clean, dry, reliable air that keeps every downstream process within its validated operating envelope.
Contact Us
Contact Person: Mia
Email: [email protected]
Tel/WhatsApp: +86 19821985894
Website: https://www.seize-air.com