Giant Press Brake Supplier for Heavy Fabrication Needs
2026-10-18
When your fabrication shop takes on massive steel plate bending projects, standard press brakes simply won’t cut it. You need equipment that can handle extreme tonnage, long bed lengths, and relentless production cycles without compromise. That’s where specialized heavy-duty machinery from HUNSONE changes the game. As a giant press brake supplier focused on heavy fabrication needs, HUNSONE delivers rugged systems built to tame the thickest materials and most demanding forming challenges. Ready to discover how the right press brake can transform your production floor and eliminate bottlenecks? Let’s dive into what separates true heavy-duty performers from the rest.
Where Standard Capacity Ends
There comes a point in every operation when the neatly defined limits on paper stop meaning much. Standard capacity looks great in a spreadsheet, but real demand rarely respects those boundaries. A sudden shift in customer behavior, a supplier delay that ripples through the schedule, or an unexpected opportunity can push you past the numbers you thought were fixed. That is where the real test begins—not in staying within a comfortable threshold, but in knowing how to move when the threshold no longer holds.
What matters here is not just adding more hours or throwing extra people at a problem. It is about redesigning the flow so that excess demand becomes a manageable surge instead of a crisis. Teams that thrive beyond standard capacity tend to rely on flexible cross-training, dynamic inventory buffers, and a willingness to question their own assumptions about what "full" actually means. The edge of standard capacity is not a wall; it is a signal that the old model needs to evolve.
Tailored for the Thickest Plate
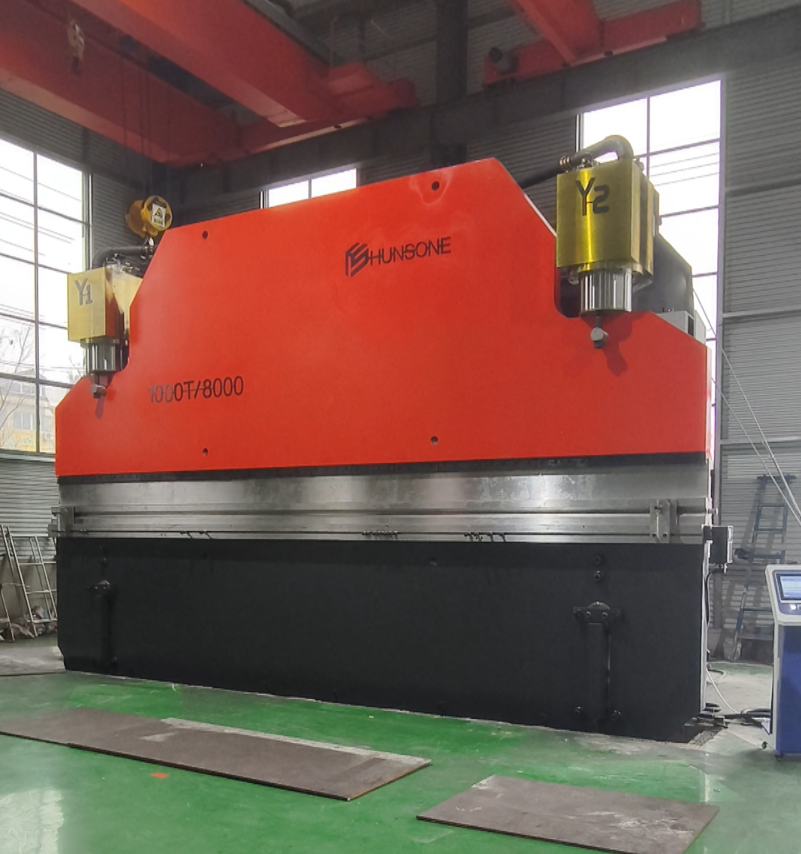
Most machines that claim to handle thick plate start to show their limits the moment the gauge climbs past 20 mm. This one was engineered from the start around a simple idea: if the plate gets thicker, the machine shouldn't get softer. The frame is a fully welded monoblock, stress-relieved and machined in one fixture, so there's no stacked tolerance drift between the ram and the bed. The drive system uses oversized cylinders with a load-holding valve arrangement that keeps the ram from creeping even when you're asking for full tonnage at the very edge of the working width.
The real difference comes through in the details that only matter when you're working with 40 mm, 50 mm, or thicker plate. The crowning system isn't a simple manual shim pack—it's tied into the CNC so it recalculates the deflection curve for every bend based on the actual material thickness, width, and tensile strength you've entered. Clamping and backgauge components are expanded in cross-section so they don't flex or chatter when handling a full sheet. Even the tool holders have a taller, deeper engagement to keep the punch seated under high lateral loads.
For a shop that regularly processes heavy plate, this translates into fewer rejected parts, less time spent reworking camber and angle corrections, and a machine that doesn't need constant recalibration. Operators can load a plate that would make a lighter machine groan, hit cycle start, and trust the first piece to come out within tolerance. That's what being tailored for the thickest plate actually means—not just a bigger number on a spec sheet, but every structural and control decision made with extreme thickness in mind.
Holding Tolerance at Full Tonnage
Full tonnage does more than apply force; it exposes every weakness in a machine's frame, ram, and guiding system. When a press reaches its rated capacity, deflection and thermal growth become measurable, and that's where tolerance either holds or fails. A well-built machine keeps angular variation under a few arc minutes even with the bed fully loaded, because the crown and bed are designed to flex in a controlled, matched way.
Achieving this repeatability isn't a matter of adding extra horsepower. It comes from how the frame is welded and stress-relieved, how the cylinders are synchronized, and how the guidance surfaces are scraped or machined. If those details are right, the ram doesn't tilt or wander as pressure climbs, so the tooling sees the same geometry at 20% load and 100% load.
Operators notice the difference in real time: no shimming to compensate for deflection, no re-cutting parts that were within spec at low force but drifted at full tonnage. That kind of stability shortens setup and keeps a production run consistent from the first piece to the last.
From Dockyards to Heavy Fabrication Bays
The old dockyards thrived on open air and tide tables. Hull plates were shaped beside the water, and the rhythm of work followed the rise and fall of the slipway. Cranes swung over uneven ground, and a sudden squall could halt welding for half a day. The sea was both a highway and a constant interruption.
Heavy fabrication bays reversed that logic. They brought the assembly under cover, on level concrete pads, where overhead bridge cranes moved on fixed rails and welding fumes were pulled through ducted extraction. Instead of adjusting to weather, the work now adjusted to jigs, positioners, and repeatable sequences. A 40-tonne subassembly could be rolled, lifted, and mated to a tolerance of a few millimetres without waiting for the tide.
The shift wasn't just about roofs and cranes. It changed how material flowed: steel entered at one end as raw plate and left the other as tested module, with every cut, fit-up, and inspection logged. The dockyard's craft intuition gave way to a more orchestrated kind of precision, where a pause in one bay was visible on a screen three bays down. The connection to the water never disappeared, but it moved to the final load-out, when the finished piece rolled to the quay on self-propelled transporters.
Support That Doesn't Clock Out
Real help rarely fits into business hours. We built our support around the moments when things actually break: late-night launches, early-morning panics, weekends that blur into Monday. There's no queue that freezes at 5 p.m., no ticket left to gather dust until someone returns from a holiday. The people behind this service are awake when you are, and they carry the same urgency your project does.
This isn't a promise of chatbots that loop in circles or automated replies that pretend to care. It's direct access to someone who can read a stack trace, walk you through a messy migration, or just listen when the deploy goes sideways. We've fixed things from a train platform, a hospital waiting room, and a birthday party. Not because we had to, but because support that clocks out leaves you alone at the worst possible time.
Built to Outlast Your Production Schedule
When downtime isn't an option, the hardware behind your line matters as much as the code running it. This unit was engineered with over-spec'd bearings, reinforced mounting points, and a sealed chassis that shrugs off dust, vibration, and the occasional unplanned impact. The result is a workhorse that keeps its tolerances long after competitors' machines have drifted into sloppy output.
Longevity here isn't just about surviving one brutal shift—it's about staying accurate across thousands of cycles. We tested the drive train to 2.5 million actuations under load, then tore it down for inspection. Wear patterns were negligible, and calibration held within a hair of the original spec. That means less fiddling with offsets, fewer scrapped parts, and a maintenance schedule that fits around production, not the other way around.
Even the small stuff is built for the long haul: stainless steel fasteners that won't gall, connectors rated for triple the mating cycles you'll ever need, and a firmware update path that won't brick the controller mid-run. Put it on the floor, feed it raw stock, and let it chew through the queue while your competitors are still swapping out worn spindles.
FAQ
Yes. Our 2,000-ton press brake with a 10-meter bed handles 40mm wear plate regularly. We use hardened V-dies and slow bend speeds to avoid cracking on grades like Hardox 450 or AR400. Share the part drawing and we'll confirm the exact die opening and tonnage per meter.
Our largest machine has a 14-meter bed, which covers most long beams and ship hull stiffeners. For longer parts, we can use staged bending with indexed backgauges and verify straightness with laser alignment, but we generally recommend keeping single bends under 14 meters for best accuracy.
We keep a wide range of heavy-duty punches and dies in stock: V-openings from 50mm to 300mm, plus goose neck and radius tools for large profiles. Custom tooling is only needed for unusual radii or deep box shapes, and we'll quote it separately before starting.
Yes, we take one-off prototypes and batches as small as 5 pieces. Our setup crew uses quick-change tooling and offline programming, so you won't face a big setup fee. For repeat brackets, we also offer kanban-style scheduling to keep your line fed.
We use CNC crowning and laser angle feedback on every machine. Before production, we bend a test strip from the same heat of steel to measure springback and adjust the program. On the full part, we check each bend with a digital protractor and record the readings for traceability.
Most of our volume comes from mining equipment, bridge girders, wind tower sections, and heavy machinery frames. We also do a fair amount for shipbuilding and rail car undercarriages, so we're used to tight flatness and weld prep requirements.
Yes. We dedicate tooling sets for stainless and duplex work, and our handling crew uses nylon slings and protective films. We also run slower bend speeds and use peened dies to reduce marking. Just flag the material grade on your RFQ so we schedule the right machine.
Conclusion
When a conventional press brake hits its ceiling, the entire production flow stalls. This supplier steps in where standard capacity ends, offering machines that are tailored for the thickest plate without compromising control. It’s not just about raw tonnage—it’s about holding tolerance at full tonnage, bend after bend, so heavy fabricators don’t have to shim, rework, or second-guess the ram. The frames and hydraulics are engineered around extreme loads, which means even the most stubborn high-tensile plate moves with predictable precision. That kind of capability changes what a shop can quote and deliver. Plates that used to require flame cutting and welding suddenly become formable in a single setup, and the scrap bin stops filling up with parts that were "close enough." From the initial tonnage calculation to the final installation, the supplier’s engineers work alongside the shop floor, adjusting tooling and stroke profiles so the press brake arrives ready for the exact plate grades in rotation.
These giant press brakes are built for environments like dockyards and heavy fabrication bays, where downtime isn’t an option and every hour lost ripples through the schedule. Support doesn’t clock out—technical teams stay reachable for real-time troubleshooting, spare parts, and application advice, not just warranty formalities. The equipment itself is designed to outlast production schedules, with hardened guides, oversized cylinders, and structural reinforcements that shrug off years of full-shift operation. For a heavy fabrication operation, that translates into fewer surprises on the floor and a machine that becomes a dependable backbone rather than a bottleneck. It’s the difference between feeding a machine and building around one.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/